The precision engineering steel structures need for accurate assembly
The precision engineering steel structures need for accurate assembly
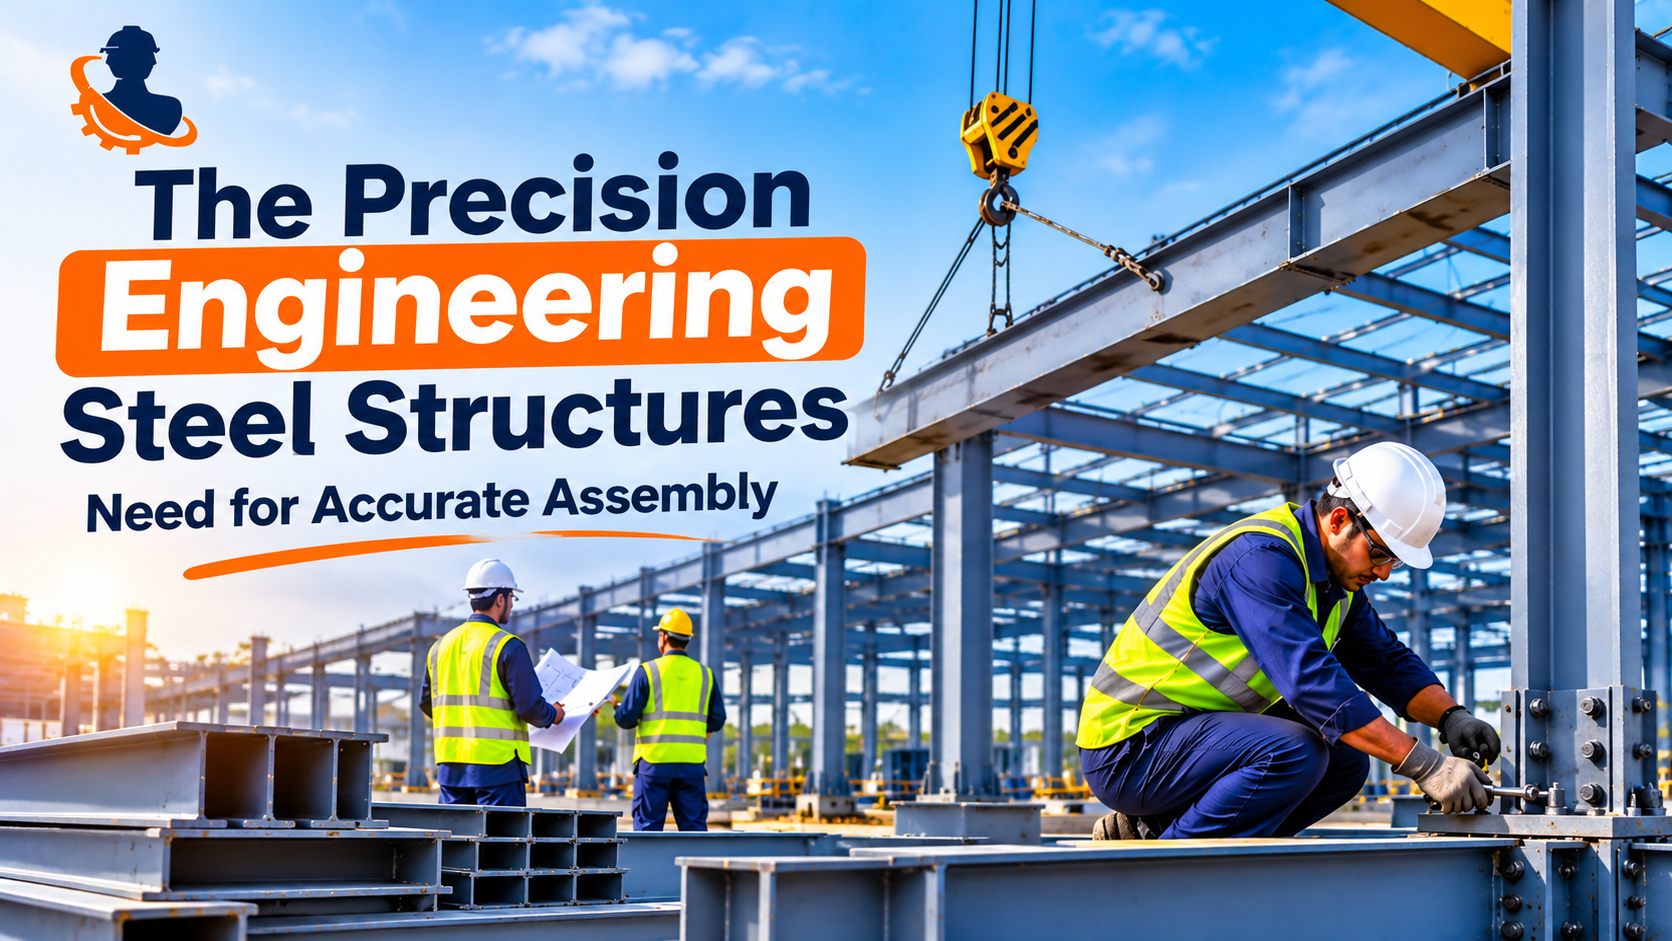
Accurate steel assembly starts with a shared set of dimensions. The designer defines where the members meet, the fabricator builds to those dimensions, and the survey team checks whether the foundations and installed steel match the same reference points. The precision engineering steel structures need for accurate assembly covers each of these steps. It also accounts for the predictable ways steel can move during welding, transport and erection. A bolt pattern can match the drawing perfectly and still miss its connection if the shop and site teams measure from different points.
What accurate assembly means on a steel project
Accurate assembly means that beams, columns, braces and connecting plates fit within the limits specified for the project. Bolts fit the approved holes, bearing surfaces seat as designed, and the erected frame meets the required checks for position, level and plumb. Each connection also needs enough working space for the crew to install and inspect it.
Fit matters beyond the steel frame. A column can stand within its permitted position and still leave too little adjustment for a cladding bracket or a piece of equipment. Design teams should identify such interfaces while they can still coordinate the geometry. Crane runway beams, façade supports and equipment platforms often need particular attention because another system depends on their alignment.
The contract drawings and specifications should identify the applicable tolerances and any tighter requirements at individual interfaces. Before fabrication, the team needs to know what it will measure, which reference it will use and when it will verify the dimension.
Start with drawings that show how parts meet
Shop drawings turn the structural design into instructions for manufacturing individual pieces. They show member lengths, hole positions, plate orientations, weld locations and piece marks. Erection drawings then show where those pieces belong in the frame and how they relate to grids, elevations and neighbouring members.
A detailer should review a connection in three dimensions, including the space a fitter needs to insert a bolt and position a tightening tool. A gusset plate may clear a beam in the model while restricting access to a nut once the adjoining brace goes in. Checking the planned erection sequence alongside the connection detail can reveal that problem while the team can still change the order of work or resolve the connection detail with the designer.
Drawing revisions also affect fit. Moving a column connection can change the beam end plate, the attached brace and the location of a secondary support. The fabrication team needs one current revision for each affected part, including any cutting or drilling files exported from the model.
Use the same reference points in the shop and on site
A datum gives the team a fixed reference from which to locate holes, plates or members. For a base plate, the critical reference may be the intersection of the column centre lines. For a beam, it may be the working point at one end and the elevation of the top flange. The drawing should identify the reference clearly enough for two inspectors to measure the part the same way.
Measuring a series of holes from one established datum limits the risk of carrying a layout error forward. If each hole takes its position from the previous one, a small error at one step can shift every hole that follows. The same principle applies to site set-out when crews locate successive bays from an established survey grid.
Teams need to account for how they support the member while measuring it. A long beam can deflect under its own weight. A measurement record that identifies the support conditions helps the site team interpret differences later.
Allow for tolerances at the connection
A tolerance defines how far a dimension may vary from its specified value. Fabrication tolerances cover features such as member length, straightness and hole location. Erection tolerances cover the position and alignment of the installed steel. The usable clearance at a connection depends on how the relevant deviations combine.
Consider a beam that fits between two columns. If both column connection faces sit slightly inward and the beam measures close to the upper limit of its permitted length, the beam may be difficult to fit even if every individual measurement passes. Checking the opening between connection faces against the measured beam length helps the team identify potential interference before the lift begins.
Engineers can specify details such as slotted holes or approved shims where the connection needs adjustment. The design must account for the direction and amount of movement available. A field crew that encounters interference should record the actual dimensions and obtain an approved resolution before altering the steel or its fastener holes.
Maintain dimensional accuracy through fabrication
Accurate fabrication starts with checking the incoming steel. Rolled sections can vary in depth, straightness and flange geometry within their permitted limits. If a connection depends on a close fit against a flange, checking the actual section before preparing the adjoining plate can prevent a mismatch.
Computer-controlled drilling and cutting help shops reproduce a verified pattern. A wrong origin or mirrored part file can produce the same mistake across an entire batch. Checking the first component against the latest drawing helps catch those errors before the shop repeats them. For paired plates, the inspector should check how the parts face each other in the assembled connection as well as verifying hole spacing.
Fitters use jigs and fixtures to locate parts such as stiffeners, cleats and end plates before welding. The fixture itself needs periodic checks. A stop that shifts during repeated use can move every plate that seats against it. Final measurements should reflect the condition of the released component after the shop removes it from the fixture.
Control weld distortion and inspect after cooling
Weld metal contracts as it cools and can pull the surrounding steel with it. An end plate may tilt, a built-up column may bow, or a beam may develop sweep. A joint that checks square during initial fit-up can therefore present a different geometry when it reaches the erection crew.
The fabrication team can manage this movement through fit-up, suitable restraint and a planned welding sequence that follows the applicable welding procedure. On a symmetrical built-up member, a balanced sequence can help limit distortion when the joint detail and procedure allow it. On an end plate, the inspection should confirm its position and angle after welding and cooling because both affect how it meets the adjoining member.
Dimensional and weld inspections answer different questions. The weld inspection checks whether the weld meets its acceptance criteria. The dimensional inspection confirms whether the member still meets the required geometry. A finished component needs to pass the applicable checks before the shop releases it for dispatch.
Trial-assemble the connections that are hardest to correct
Trial assembly brings selected members together in the workshop to check their fit before dispatch. It is particularly useful for complex truss nodes, multi-member splices and assemblies made in shipping sections.
The shop can check whether mating holes align, whether a pin or bolt can pass through the connection, and whether the finished geometry matches the agreed reference dimensions. A useful trial also checks access. The team may find that a plate fits into position but leaves too little room to install the fastener after a neighbouring component goes in.
When the shop checks members as a matched set, it can use match marks and link them to the erection drawings. This tells the site team which faces or ends belong together. Recording the checked dimensions and the member orientation makes the trial assembly record useful when the crew sets out the connection on site.
Check foundations before the first lift
An as-built survey can identify anchor positions that differ from the base plate layout before a column arrives at the lifting point. Using the agreed grid and level references, the survey team checks the anchor group location, spacing, orientation and projections. It can also capture the supporting surface or bearing elevations that affect column level.
The civil and steel teams should compare the survey with the approved base plate details. An anchor group may have the correct spacing within the group and still sit off the column grid. A group may also be centred correctly while an individual anchor sits too close to the edge of its hole. Checking each anchor as well as the group location helps distinguish between those problems.
Compare the foundation survey with the dimensions of the fabricated base plates early enough for a review before erection. If there is a mismatch, the actual coordinates and plate dimensions give the engineer the information needed to assess the interface and detail a suitable correction.
Check alignment as erection moves from bay to bay
The erection sequence determines when surveyors can check the frame safely and when the crew can still make the adjustments permitted by the connection details. The first stable section gives the site team a practical point at which to verify grid position, elevations, column plumb and bay dimensions against the survey control. Subsequent measurements can reveal whether the frame is gradually moving away from its intended position.
The survey record should identify the stage of erection. Readings can change as the crew adds bracing, completes connections or transfers load from temporary supports. Temperature can also affect measurements across long runs of exposed steel. Where that movement matters to the specified tolerance, the team can record conditions and follow the project’s measurement procedure.
At a tight connection, survey information helps the crew distinguish a local fabrication mismatch from a frame alignment issue. A beam that appears too long may fit once the team confirms the positions of the supporting columns and resolves an earlier set-out deviation.
Use inspection records to resolve fit problems quickly
Inspection records are most useful when they link a measurement to a piece mark, a drawing revision and a reference point. A report that lists the measured hole centres relative to the splice face, identifies both pieces and shows their orientation makes it easier to trace the difference.
The inspection plan can set checks at stages when the team can still see or measure the critical feature. For a welded plate assembly, that might mean confirming plate location at fit-up and checking the same reference again after cooling. For a connection with coated components, it might mean verifying that the specified finish leaves the required fit at the mating surfaces.
Handling also affects accuracy. Transport supports should suit the shape and stiffness of the member, especially when it has projecting plates or slender elements. A delivery inspection can identify bending or damage before the piece leaves the laydown area.
Decide where tighter control pays off
Extra measurement has the most value where a deviation affects several trades or where access makes rework difficult. A standard beam in a repetitive bay may need routine sampling under the inspection plan. A transfer truss splice above an operating production line may justify a documented trial assembly and a more detailed site survey before the lift.
Rank interfaces by the consequences of a mismatch and by the time available to correct one. Where a column carries a crane runway bracket, for example, the team can check the bracket elevation and position in the shop, then verify the relevant alignment once the supporting frame reaches the erection stage specified for the survey. Project teams can use those findings to prioritise measurement time, plan the order of inspections and budget for any trial assembly the critical connections require.
Conclusion
For Sarojini Group, accurate steel assembly is a shared responsibility across detailing, fabrication and erection. The most valuable checks follow the connection across those stages, from the drawing datum to the fabricated member and finally to its position in the frame. When each team measures the features that govern fit and shares the results in time, it can address discrepancies while access is available and the affected work can still be adjusted.
FAQs
Why can steel members fail to fit when their dimensions are within tolerance?
Permitted deviations can add up in the same direction. For example, both supporting columns may sit slightly inward while the beam between them measures near the upper limit of its length tolerance. Each component may pass its own check, yet the available opening may leave too little clearance for the beam.
When should fabricators carry out a trial assembly?
Trial assembly is most useful for complex or critical connections, such as segmented trusses, multi-member splices and connections with restricted access. The team should check parts at a fabrication stage that represents their final fit. This lets it verify mating geometry, fastener access and piece orientation before dispatch.
What should the site team check before erecting steel columns?
The site team should verify anchor positions, spacing, orientation and projection, along with the relevant supporting elevations. It should compare those survey results with the approved base plate details using the agreed grid and level references. A documented comparison gives the project team time to resolve discrepancies before lifting starts.
NEWSLETTER
Sign up your mailing list to get lastest Updates.